How to Choose Between CHS, SHS, and RHS Hollow Sections for Structural Applications Under AS/NZS 1163
Selecting the right hollow section profile is one of those decisions that looks simple on paper and becomes complicated in practice. The three AS/NZS 1163 profiles — circular hollow sections (CHS), square hollow sections (SHS), and rectangular hollow sections (RHS) — each have genuine structural advantages in the right context and genuine disadvantages in the wrong one. Getting the choice right from the start avoids the rework that comes from changing profile mid-design when a connection detail doesn’t work or a section proves harder to procure than expected.
Load direction: the first filter
The clearest structural distinction between the three profiles is how they carry load relative to direction.
CHS has a uniform second moment of area about any axis through the centroid. This means its bending resistance and stiffness are the same regardless of which direction the load comes from. For columns in multi-storey frames, space frame nodes, and lattice members where load can arrive from multiple directions, this isotropy simplifies analysis and avoids the need to check that the section is oriented correctly relative to the applied force.
SHS also has equal section properties in both principal axes, but the values are different from a CHS of similar outer dimension because the corner radii reduce the effective section modulus compared to a sharp-cornered equivalent. For most purposes, SHS behaves like CHS in terms of axis symmetry — it doesn’t matter which face is “up” — and it’s often preferred over CHS when flat faces simplify connections.
RHS has unequal section properties in the two principal axes. The major axis (through the larger outer dimension) has a significantly higher second moment of area than the minor axis, which is deliberately used to carry bending loads efficiently when the dominant load direction is known. An RHS beam carrying vertical gravity load should be oriented with the larger outer dimension vertical. Rotating the same RHS 90 degrees reduces its bending capacity about the loaded axis by a factor that can exceed 2:1 for high-aspect-ratio sections.
If load direction is variable or unknown, CHS or SHS. If the primary bending axis is fixed and efficiency matters, RHS with the larger dimension in the primary bending direction.
Connection geometry: the practical constraint
Load direction tells you which profile is structurally most efficient. Connection geometry often determines which is practically feasible.
CHS-to-CHS connections — particularly in trusses and space frames — require profiled (saddle-cut) weld preparation where the joining member end is cut to match the curve of the chord. This is done routinely in fabrication shops with CNC profiling equipment, but it adds fabrication time and cost relative to flat-face connections. For smaller or simpler projects without access to profiling equipment, the fabrication of CHS-to-CHS joints is more labour-intensive.
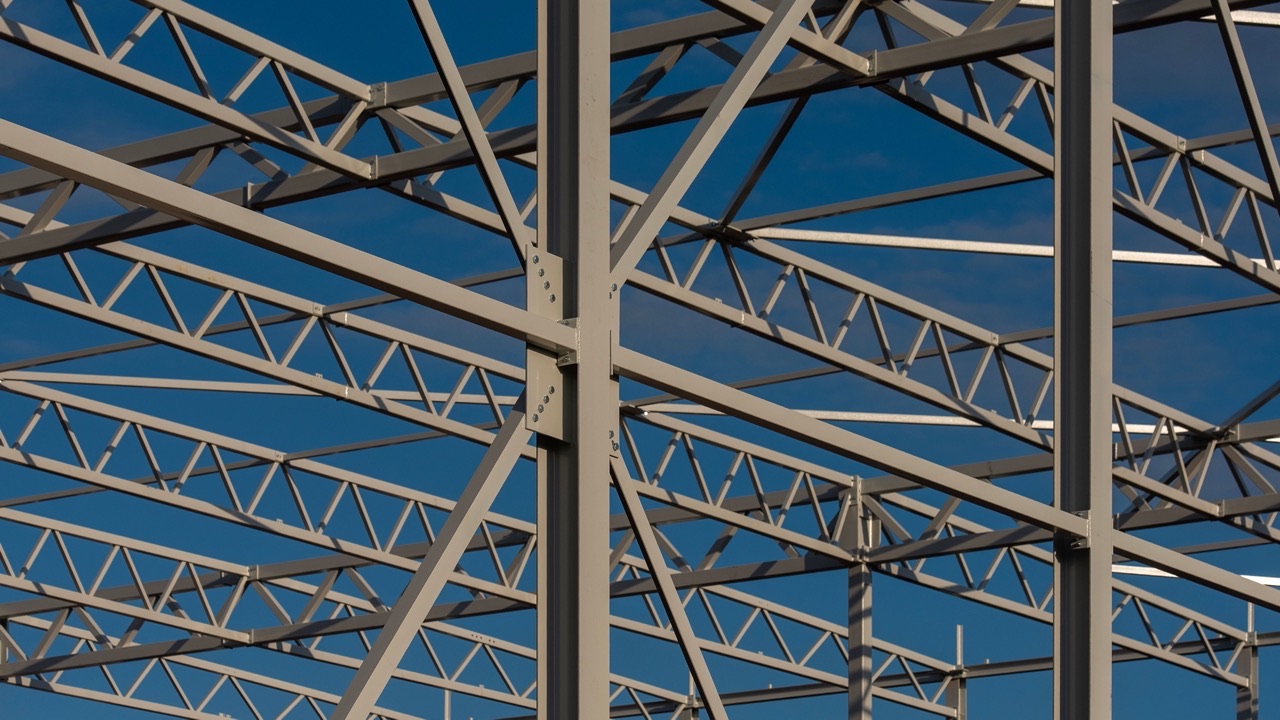
SHS and RHS connections are typically flat-face welds or bolted end-plate connections, which are faster to prepare. The flat face allows a cleat or fin plate to be fillet welded with no complex geometry. Through-bolts, baseplate connections, and splice connections are also simpler to detail on flat-face sections. For most secondary structures, platforms, handrails, and light frames, SHS or RHS is the practical default for this reason.
When hollow sections connect to other hollow sections — particularly in Vierendeel trusses or similar moment frames — the connection capacity (often governed by the chord face plastification or punching shear mechanisms) varies between CHS, SHS, and RHS. The design guides for hollow section connections (CIDECT series) treat CHS and RHS/SHS connections separately with different capacity formulae.
Architectural and aesthetic requirements
For architecturally exposed structural steel (AESS) — where the steel is visible and the finish quality matters — profile choice is partly an aesthetic decision.
CHS gives a smooth, continuous profile with no flat faces or visible corner radii, which reads as more refined in exposed applications. It’s the standard choice for columns and tie rods in high-specification architectural work: public buildings, shopping centres, transport hubs. The circular profile also avoids the dirt and water trapping that occurs at the flat faces and corners of SHS and RHS in exposed outdoor applications.
SHS gives a clean geometric appearance with four equal faces, which works well in grid-based architectural compositions and where connections are visible at both principal axis directions equally. RHS can look bulkier in some orientations but provides a clear visual cue about the structure’s spanning direction.
For unexposed structural steel — behind cladding, in mechanical spaces, in industrial buildings — aesthetic considerations don’t apply and the choice is made purely on structural efficiency, connection practicality, and procurement availability.
Availability and procurement lead time
Not all sizes within each profile are equally stocked in the Australian and New Zealand market. Common sizes of RHS (e.g., 150 × 100 × 6.0, 200 × 100 × 6.0) and SHS (e.g., 100 × 100 × 5.0, 150 × 150 × 6.0) are routinely held in distributor stock and available on short lead times. Less common sizes — very large CHS, thin-walled large RHS, or low-demand wall thickness combinations — may require mill orders with lead times of several weeks.
Specifying a section size that is not a common stock item in the local market creates procurement risk, particularly on fast-track projects. For preliminary design, it’s worth checking local distributor stock lists before committing to an unusual size. If multiple section sizes could satisfy the structural requirement, choosing the one that’s commonly stocked reduces delivery risk and often reduces cost through scale of production.
Selecting grade alongside profile
Under AS/NZS 1163 hollow sections, the standard grade for most structural applications is C350L0, providing a minimum yield strength of 350 MPa with Charpy impact testing at 0°C. C250L0 (250 MPa minimum yield) is available but less commonly specified for new structural work since C350L0 is the default grade most distributors carry. C450L0 (450 MPa minimum yield) is used where weight reduction is the priority and the higher cost per tonne is offset by material savings.
Grade affects section capacity and therefore size selection. Designing to C350L0 and then procuring C250L0 — or accepting a substitution without rechecking capacity — is a structural nonconformance. Whatever grade is used in the design calculation must be explicitly stated in the specification and verified against the Mill Certificate at delivery.